


Fully Welded Full Bore Ball Valve Q361F-16C
Full-bore butt-weld ball valve with worm gear drive for DN250–DN350 main-line isolation. Q235 fully welded body, 304 stainless ball, C+PTFE seats — zero added pressure drop, PN16 rated, shell tested to 2.4 MPa. Worm gear actuator with PTFE thrust bearing and A105 connecting plate converts high stem torque into manageable handwheel effort without gearbox sizing guesswork. Designed to GB/T30818, butt-weld ends per GB/T9113.1, rated -25°C to 120°C on water, steam, and oil. Fully welded construction — no body joints, no body gaskets, no leak paths to revisit.
- Design Pressure: 1.6 MPa
- Shell Strength Test Pressure (Water) : 2.4 MPa
- High-Pressure Sealing Test Pressure (Water):1.8 MPa
- Low-Pressure Sealing Test Pressure (Air) : 0.6 MPa
- Working Temperature: -25°C to 120°C
- Applicable Medium:Water, Steam, Oil products, etc.
Technical Specifications
Technical Requirement
| Design & Manufacture | Face-to-Face Length of Valve | Butt-Welding Connection of Valve | Inspection & Pressure Test | Temperature-Pressure Rating |
|---|---|---|---|---|
| GB/T30818 | As per drawing regulations | GB/T9113.1 | GB/T26480 | GB/T12224 |
Performance Specifications
| Design Pressure | Shell Strength Test Pressure (Water) | High-Pressure Sealing Test Pressure (Water) | Low-Pressure Sealing Test Pressure (Air) | Working Temperature | Applicable Medium |
|---|---|---|---|---|---|
| 1.6MPa | 2.4MPa | 1.8MPa | 0.6MPa | -25~120°C | Water, Steam, Oil products, etc. |
Material of Components
| No. | Component Name | Material | No. | Component Name | Material |
|---|---|---|---|---|---|
| 19 | Worm Gear Actuator | Assembly | 9 | Thrust Bearing | PTFE |
| 18 | Parallel Key | 45 | 8 | Upper Stem | 20Cr13 |
| 17 | Packing Pressure Ring | 20Cr3 | 7 | Ball | 304 |
| 16 | Connecting Plate | A105 | 6 | O-Ring | Fluororubber |
| 15 | O-Ring | Fluororubber | 5 | Valve Seat | C+PTFE |
| 14 | Packing Gasket | C+PTFE | 4 | Fireproof Ring | Q235+ENP |
| 13 | Standard Spring Washer | 65Mn | 3 | Spring Washer | ss321 |
| 12 | Hex Nut | 25 | 2 | Valve Body | Q235 |
| 11 | Stud Bolt | 35 | 1 | Left/Right Body | Q235 |
| 10 | Sliding Bearing | 25+Tin Bronze+PTFE |
Main Shape Size and Connection Size
| DN | L | D | Dmin | A |
|---|---|---|---|---|
| 250 | 730 | 273 | 250 | 426 |
| 300 | 850 | 325 | 300 | 510 |
| 350 | 980 | 377 | 350 | 590 |
Technical Drawings
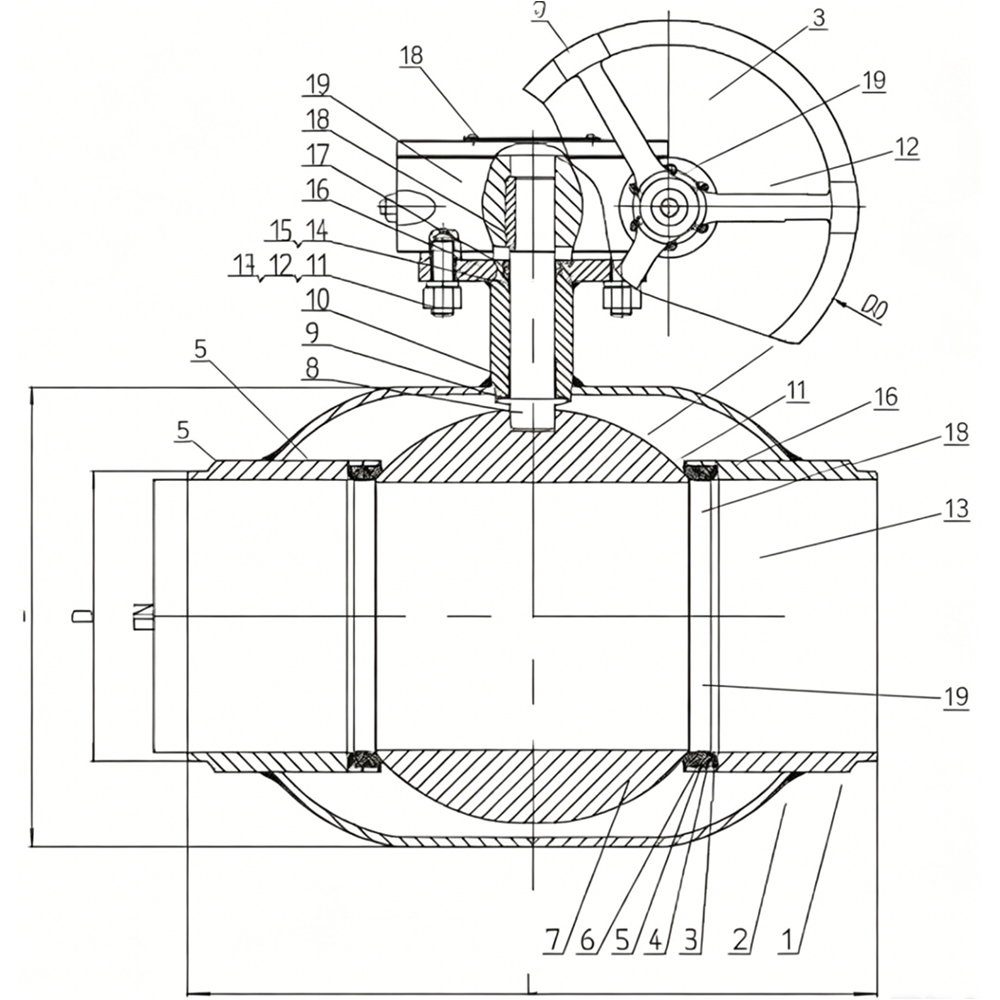
Core Features & Advantages
1. Full Bore, Fully Welded Ball bore equals pipe ID — zero flow restriction, zero added pressure drop, piggable without special provisions. The Q235 body is single-piece forged and welded: no body bolts, no body gaskets, no leak paths from the envelope.
2. Worm Gear with PTFE Thrust Bearing Worm gear actuator mounted via A105 connecting plate converts high stem torque at DN250–DN350 into light handwheel effort. PTFE thrust bearing under the upper stem absorbs axial load so the gear train sees only rotary resistance — smooth operation without gear bind.
3. 304 Ball, C+PTFE Seats, Fire-Safe Ring 304 stainless ball on carbon-reinforced PTFE seats seals bidirectionally at PN16. Q235+ENP fire-safe ring is standard — if the soft seats are lost, secondary metal-to-metal contact holds the line.
4. Designed to GB/T30818, Butt-Weld Ends Shell tested to 2.4 MPa water, seat tested to 1.8 MPa water, low-pressure air seal at 0.6 MPa. Butt-weld ends per GB/T9113.1 match pipe schedule directly — no flange adapters, no gasket inventory, no alignment hardware.
5. DN250–DN350, One Platform Same seat material, same stem seal, same bolt pattern across all three sizes. One spare parts family, one gearbox maintenance procedure, one training session for the crew.
Applications
- District heating transmission main-line isolation
- Steam header and main distribution isolation
- Industrial cooling water mains
- Oil product pipeline block valves
- Water treatment plant main headers
- Fire water ring main isolation
- Pump station suction and discharge isolation
- Pipeline pigging sections — full bore, no obstructions
Why Choose Fully Welded Full Bore Ball Valve Q361F-16C?
1. Full Bore Without the Weight Penalty Ball ID equals pipe ID — the flow path has no restrictions, no added pressure drop, and a pig passes clean through. You get full-bore performance without upsizing the entire valve envelope.
2. Worm Gear That Just Works Gear drive with PTFE thrust bearing absorbs axial stem load before it reaches the gear teeth. A105 connecting plate bolts directly to the valve — no adapter, no custom bracket. The handwheel turns light across the full DN250–DN350 range.
3. Weld It, Forget It Butt-weld ends plus a fully welded Q235 body. The valve goes inline as a permanent pipe section — hydrotest it, bury it, insulate it. No flange torque checks, no body gasket replacements, no maintenance schedule for the pressure boundary.
4. One Platform, Three Sizes DN250, 300, 350 — same seats, same seals, same gearbox procedure. One spare parts kit covers the main-line inventory. One training session for the entire crew.
A main-line valve that disappears into the pipe after hydrotest — no bolted joints to maintain, no bore reduction to compensate for, no gearbox to fight.


